
The BUG-O MM-1 is a programmable pipe cutting machine for automated cutting of profiles, holes and shapes on pipe. It uses a two-axis system that rotates the pipe with a three-jaw chuck while moving the cutting torch along the pipe axis.
With 4″ to 16″ pipe diameter capacity, oxy-fuel or plasma process compatibility, pre-programmed saddle, offset saddle, lateral, miter and hole cuts, custom irregular shape programming, 0 to 3 rpm speed range and 1600 lb / 726 kg pipe weight capacity, the MM-1 is a practical mechanised solution for repeatable industrial pipe cutting.
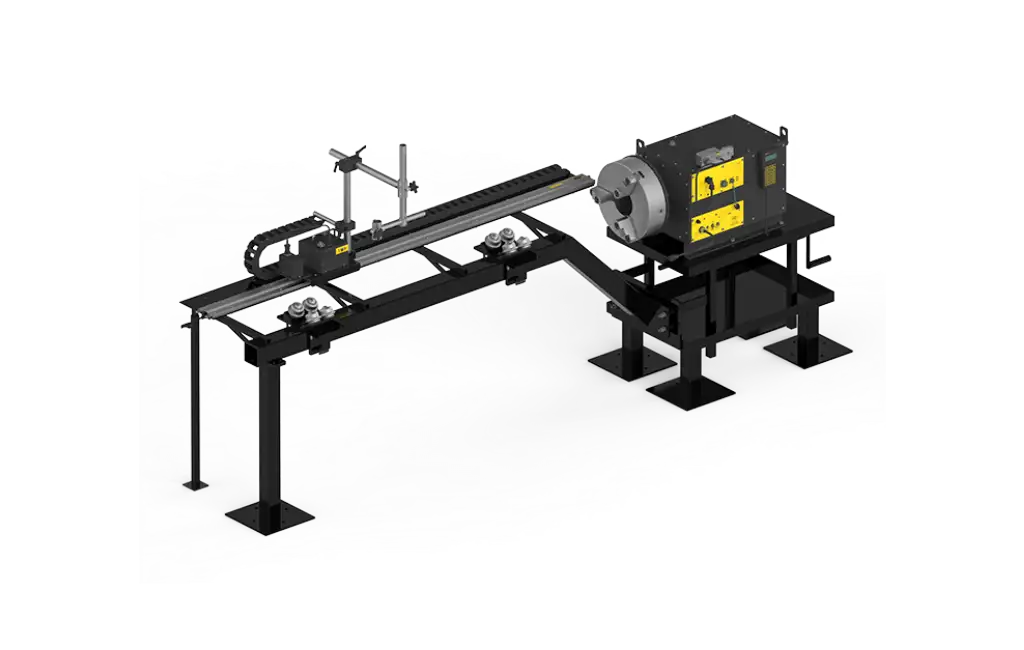
The BUG-O MM-1 is a programmable pipe cutting machine designed to automate the cutting of profiles, holes and shapes on pipe. It is a computer-controlled, two-axis mechanised system that rotates the pipe on a roller bed with a three-jaw chuck while simultaneously moving the cutting torch back and forth along the pipe axis.
The MM-1 is designed for pipe diameters from 4″ to 16″ / approximately 100 to 406 mm and can be configured for oxy-fuel or plasma cutting. Instead of relying on templates, manual layouts or time-consuming calculations, the operator selects the required cut type from the menu, enters the pipe data and starts the programmed cutting cycle.
Pre-programmed shapes include saddle cuts, offset saddle cuts, laterals, miter cuts and holes. Irregular shapes can also be plotted, programmed and saved for future use, making the MM-1 a practical solution for pipe fabrication teams that need repeatability, speed and reduced layout time.
The main technical advantage of the BUG-O MM-1 is that it combines pipe rotation and torch-axis movement into a coordinated two-axis programmable cutting system. This allows the machine to produce pipe profiles and shaped openings that would otherwise require manual layout, templates, calculations and highly skilled freehand cutting.
The three-jaw chuck rotates the pipe while the cutting torch travels along the pipe axis. This coordinated movement allows the MM-1 to cut common pipe fabrication shapes such as saddles, offset saddles, laterals, miters and holes with repeatable geometry.
The pre-programmed cut menu reduces setup complexity. The operator selects the cut type, enters the required pipe diameters and starts the cutting sequence. This improves workflow efficiency and reduces the risk of manual layout errors.
The ability to plot, programme and save irregular shapes gives the MM-1 additional production flexibility. Once a custom shape has been programmed, it can be stored for future use, supporting repeat orders and recurring fabrication requirements.
The MM-1 can also be configured for either oxy-fuel or plasma cutting. This gives the buyer flexibility to select the cutting process according to material, thickness, existing workshop equipment and production requirements.
The BUG-O MM-1 is designed for pipe fabrication environments where profiles, holes and shaped pipe cuts must be produced accurately and repeatedly. It is suitable for cutting saddles, offset saddles, laterals, miter cuts, holes and irregular programmed shapes.
Typical applications include pipe fabrication, structural pipe work, industrial piping, sprinkler pipe preparation, process piping, vessel and pipe connection preparation, workshop production, repetitive pipe profiling and fabrication jobs where manual layout would slow production.
The MM-1 is especially useful where repeatability matters. By removing the need for manual templates and layout calculations, it supports faster production, more consistent cuts and easier repeat work across similar pipe components.
The MM-1 is a strong choice for companies that need to move from manual pipe layout and cutting toward a more repeatable, programmable process. It is not simply a pipe rotator or a torch carriage; it is a coordinated pipe cutting system that automates both pipe rotation and torch travel.
For fabrication teams, the commercial value is reduced layout time, reduced dependence on manual calculation, improved cut repeatability and better production consistency. The operator can call up standard cut types from the menu and store irregular shapes for future use, which helps reduce repeated setup work.
For companies cutting pipe profiles regularly, the MM-1 can improve throughput and process control while helping reduce human error. Its ability to work with oxy-fuel or plasma also makes it adaptable to different cutting strategies and workshop requirements.
| Product | BUG-O MM-1 |
|---|---|
| Product type | Programmable pipe cutting machine |
| Machine type | Computer-controlled mechanised pipe cutting system |
| Axis configuration | 2-axis programmable machine |
| Primary use | Automated cutting of profiles, holes and shapes on pipe |
| Cutting processes | Oxy-fuel or plasma cutting |
| Cutting diameter, product page | 4" - 16" / 102 - 406 mm |
| Cutting diameter, manual technical data | 4" - 16" / 100 - 400 mm |
| Pipe length capacity, product page | 3' - 38' pipe length stated on page. The page also lists 76 mm - 11.6 m, but 3 ft converts to approximately 914 mm, so the metric minimum should be verified before publishing. |
| Pipe weight capacity | 1600 lb / 726 kg |
| Speed range, product page | 0.2 - 3 rpm |
| Speed range, manual technical data | 0 - 3 rpm |
| Pipe holding system | Three-jaw chuck |
| Pipe support | Roller bed with roller block assemblies |
| Cutting motion | Pipe rotates on roller bed while cutting torch moves back and forth along the pipe axis |
| Pre-programmed cut types | Saddle cuts, offset saddle cuts, lateral cuts, miter cuts and holes |
| Custom shape capability | Irregular shapes can be plotted, programmed and saved for future use |
| Programming method | Programming pendant control; Windows-based software also available |
| Power requirement | 120 VAC / 50-60 Hz / 1 phase or 240 VAC / 50-60 Hz / 1 phase |
| Net weight | 550 lb / 250 kg |
| Shipping weight | 750 lb / 340 kg |
| Overall length | 137" / 3480 mm |
| Overall width | 36" / 914 mm |
| Overall height | 55" / 1397 mm |
| Major shipped components | Adjustable table and headstock, drive carriage, standard arm assembly and two roller block assemblies |
| Oxy-fuel setup note | Uses a three-hose cutting torch with hoses routed to the quick-action manifold |
| Plasma setup note | Equipped with rotary ground, contact relay and holding clamp for plasma torch when configured for plasma cutting |
| Standard arm assembly | SEO-3350 MM-1 Standard Arm Assembly |
| 24" capacity standard arm assembly | SEO-3350-24 MM-1 24" Capacity Standard Arm Assembly |
| 8' bed extension | SEO-3390 MM-1 8' Bed Extension |
| 24" capacity 8' bed extension | SEO-3390-24 MM-1 24" Capacity 8' Bed Extension |
| Roller block assembly | SEO-3590 Roller Block Assembly |
| Headstock assemblies | SEO-4550 / SEO-4552 MM-1 Headstock |
| Encoder assembly | CWO-3730 Encoder Assembly |
| Cabinet assembly | CWO-3985 Cabinet Assembly |
| Motor assembly | CWO-9440 Motor Assembly |
| Hand-held terminal | BUG-6050 Hand Held Terminal |
| Control panel assemblies | CBO-4160 for 120 VAC; CBO-4162 for 240 VAC |
| Remote pendant | CBO-4170 MM-1 Remote Pendant |
| Pendant cable | CBO-4171-__ MM-1 Pendant Cable |
| Interconnecting wiring harness | CBO-4119 |
| Encoder wiring harness | SEO-4123 |
| Country of manufacture | USA |
MM-1

Fill out the form below, and we will be in touch shortly.
